Dairy plant water and energy: CIP, refrigeration, steam and reuse in one view
 Milvian AI teamFacilities and infrastructure intelligence
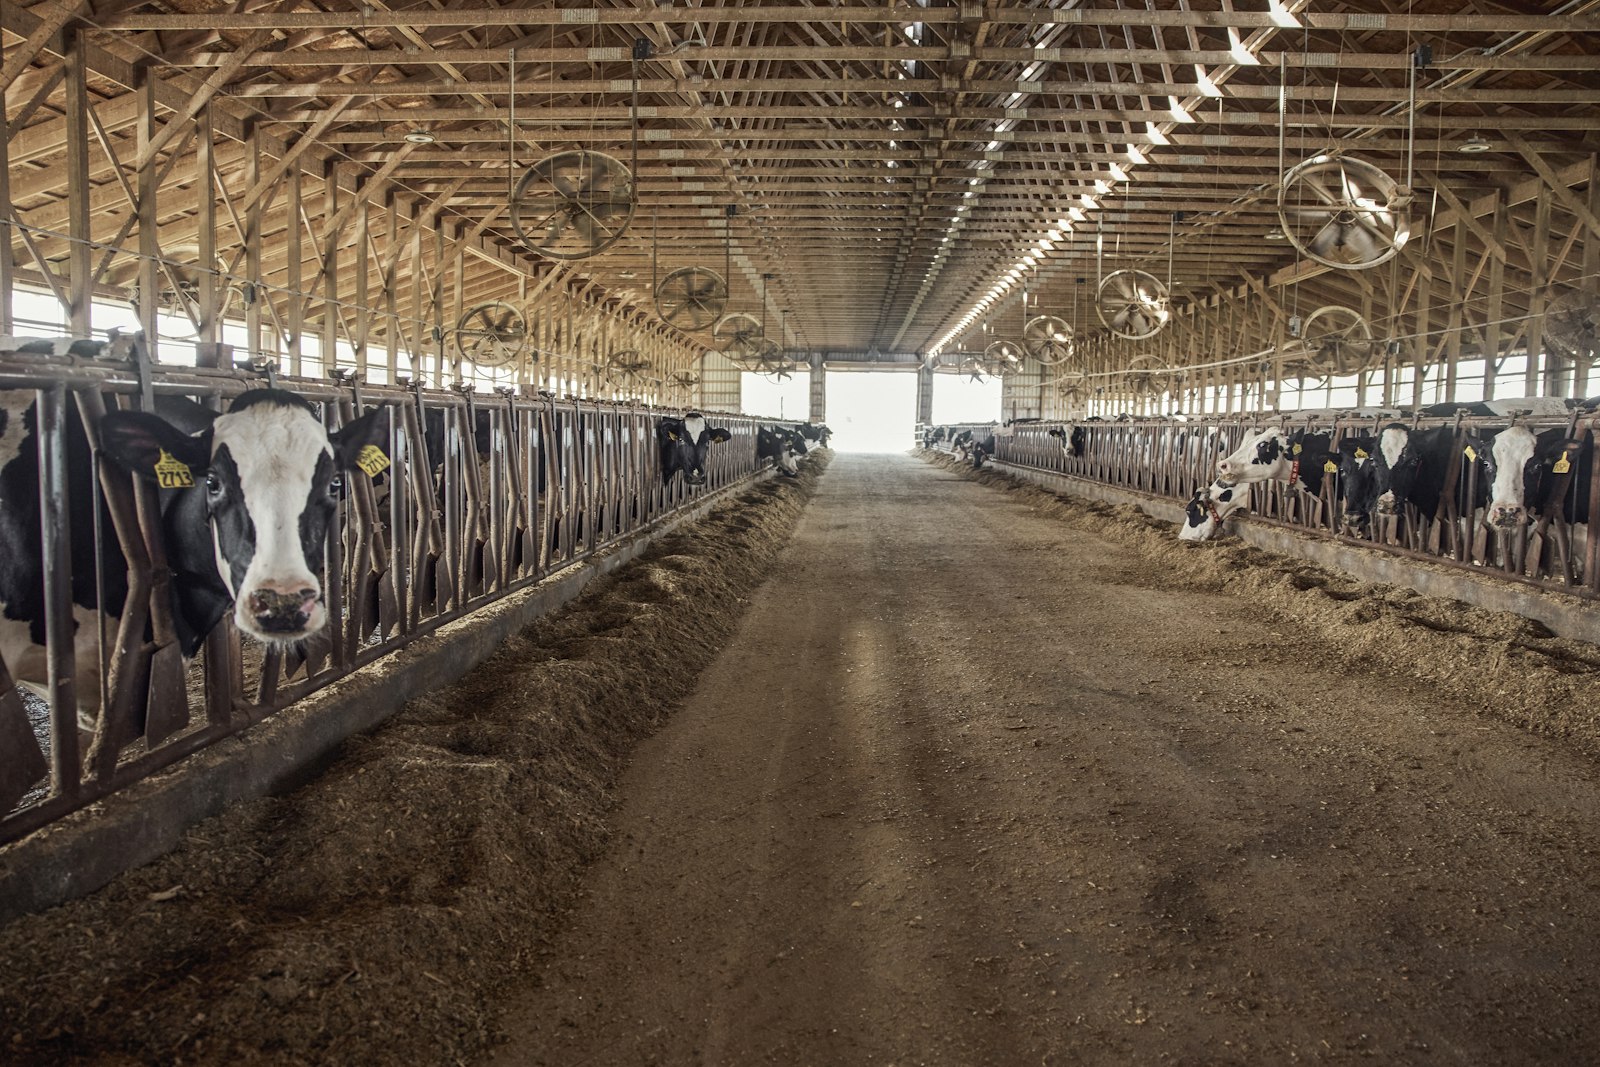
Dairy plant water and energy management is measuring and reducing the water, electricity, gas and steam a dairy uses across receiving, processing, cleaning, refrigeration and wastewater treatment. Aqueduct supports it by sub-metering each process area, baselining use against production and weather, tracking reuse and treatment efficiency, routing fixes to the CMMS and verifying each saving.
Why dairy is a water and energy business
Milk is mostly water, and almost every step that turns it into a product uses more water and energy. It is cooled the moment it leaves the cow, heated to pasteurize it, cooled again, sometimes concentrated or dried, and stored cold. Between every batch, the equipment it touched is cleaned with hot water and chemicals. A dairy plant is a heat exchanger, a refrigeration plant and a cleaning operation wrapped around a product line.
That makes water and energy two of the largest controllable costs in dairy, and they are tightly linked. Hot water for cleaning uses gas or steam. Refrigeration rejects heat that could warm water. Wastewater carries away product that was paid for, plus heat and chemicals. Treating water and energy as separate budgets hides the connections where most of the savings are.
Major dairy operations run on Aqueduct, and the pattern across them is consistent: the first gains come from measuring each process area separately, finding the cycles and equipment that use more than the product requires, and verifying each change at the meter.
Where water and energy go in a dairy plant
Clean-in-place, or CIP, is usually the largest single water use. Each cycle runs a pre-rinse, a caustic wash, an intermediate rinse, often an acid wash and a final rinse, with hot water and chemical dosing at each stage. CIP volumes and temperatures are set during commissioning and then rarely revisited, even when products, schedules and line lengths change.
Refrigeration is typically the largest electricity load. Ammonia or other refrigerant systems cool raw milk, product and cold stores, with compressors running around the clock. Compressor sequencing, condenser performance and defrost cycles all move the energy bill. Boilers and steam serve pasteurization, CIP heating and, in powder plants, evaporators and dryers. Compressed air, pumps and homogenizers make up much of the rest.
Wastewater closes the loop. Dairy effluent carries milk solids, fats and cleaning chemicals, so it usually needs pretreatment before discharge or treatment on site. Every liter of product lost to drain raises both the treatment load and the cost of the milk that was paid for. On the farm side, milking parlor washdown and plate coolers add their own water and energy uses.
Dairy process areas and what to meter
Each area has its own driver, and its own sign of waste.
| Area | Main water and energy use | What to meter and watch |
|---|---|---|
| Receiving and storage | Silo cooling, tanker washing | Water per tanker wash, silo refrigeration power |
| Pasteurization | Heating and cooling, regeneration | Steam or hot water input, chilled water, product flow |
| CIP | Hot water, caustic and acid solutions, rinses | Water and heat per cycle, by circuit and line |
| Refrigeration | Compressors, condensers, cold stores | Compressor power, run hours, suction and discharge conditions |
| Boilers and steam | Gas, make-up water, condensate | Gas per unit of steam, condensate return, make-up water |
| Wastewater and reuse | Pretreatment, STP, RO recovery | Inlet and treated flow, treatment efficiency, RO recovery and reject |
Measure per cycle, per line, per unit of product
A single water meter at the plant entrance cannot tell a long CIP cycle from a leaking valve. The first step is sub-metering the areas that matter: CIP supply by circuit, boiler make-up, refrigeration condensers, the main production halls, and the wastewater inlet and outlet. Existing meters with pulse outputs connect through LoRaWAN pulse counters, Modbus and M-Bus meters connect through bridges, and camera meters can read older meters without replacing them. Installation runs through partners.
Once areas are metered, normalize. Water and energy per unit of product is the number that matters, because a busy week should use more than a quiet one. Aqueduct baselines each line by regression on historical use plus cooling and heating degree days, and the same model can be read against production volume so a rise in output is not mistaken for waste. Uploading 6 to 12 months of utility bills gives a baseline on day one.
Per-cycle data is where CIP savings appear. When each cycle's water and heat are visible by circuit, cycles that run longer than validated, rinses that overshoot and circuits cleaned more often than required stand out. Changes to cleaning procedures must stay within the plant's food safety plan and be validated by its quality team. Aqueduct supplies the evidence for that conversation.
Refrigeration and the energy behind cold
Refrigeration runs every hour of the year, so small inefficiencies compound. Compressors that short cycle, condensers fouled with scale or debris, defrost cycles set on timers rather than need, and cold store doors left open all add load. Aqueduct reads compressor power and, where field devices allow, suction and discharge conditions, so performance can be compared with the expected profile for the outdoor conditions.
Peak demand matters too. Starting refrigeration, homogenizers and large pumps at the same moment can set a monthly demand peak in a single interval. EnergySmart shows interval demand and load sequencing options, so loads can be staggered to stay under the plant's allotted demand. Power factor correction reduces the extra current poorly loaded motors draw.
As vibration and acoustic sensing is added to rotating equipment, early signs of failure on compressors and pumps, such as rising vibration, a new sound signature or a drift in energy use, can schedule maintenance before a breakdown spoils product. Where control is enabled, with owner approval, schedules and setpoints can be adjusted through BACnet or Modbus field devices, with every command logged.
Water reuse, treatment and recovery
Dairy plants have unusual reuse opportunities. Plants that evaporate milk or whey recover large volumes of condensate from the product itself, and that water can be treated, often with reverse osmosis, for reuse in cleaning, boilers or cooling. On farms, water warmed in plate coolers is commonly reused for livestock drinking water or washdown. Final CIP rinses can often be recovered as pre-rinse for the next cycle.
Reuse only pays if it is measured. Aqueduct's water digital twin is built block by block to match the plant, including RO units and sewage or effluent treatment plants where they exist. It shows RO feed, permeate, reject and recovery, and STP inlet, treated flow and efficiency, alongside the rest of the water balance, refreshed every 60 seconds.
Treatment efficiency is a key requirement in plants that run their own STP or RO. A drop in RO recovery or STP efficiency means more fresh water bought and more effluent discharged. Seeing it the day it starts, rather than at the next lab report, lets the team act before the cost builds.
Act, verify and report
Each finding becomes a ticket in the plant's CMMS with the area, the evidence and a recommended fix. Aqueduct does not replace the CMMS or the plant's control systems. Technicians, work orders and parts stay where they are, and control of process equipment stays with the plant's own systems unless the owner enables it.
Verification makes savings bankable. A shorter CIP rinse, a recovered condensate stream or a repaired compressor is counted only when the meter shows use below the baseline. That verified result becomes the new baseline. Each plant's result with Aqueduct is verified at the meter against a weather-normalized baseline.
The same data supports sustainability programs, customer requests and certifications that ask for water and energy performance, which the plant or its consultant files. Aqueduct provides the metrics.
Where to start in a dairy plant
Start where the water and energy are largest and the meters are easiest to reach: the main water supply, boiler make-up, CIP supply and the wastewater inlet, plus the refrigeration plant's electricity feed. Upload 6 to 12 months of utility bills so the baseline is ready on day one, and check the device health view to confirm every meter reports reliably before drawing conclusions from it.
In the first weeks, look at three things. Water used when production is stopped, which points to leaks, open hoses and valves that do not seal. CIP water and heat per cycle by circuit, which shows the cycles worth reviewing with quality. And refrigeration power against outdoor conditions, which shows compressors and condensers that have drifted from their expected profile.
Then make it a routine. A short weekly review of the areas running above baseline, the treatment efficiency trend and the tickets routed to the CMMS keeps the gains from slipping back as products, shifts and seasons change.